
PA12 Nylon Guide: Properties, Limits and Uses of Nylon 12 in SLS
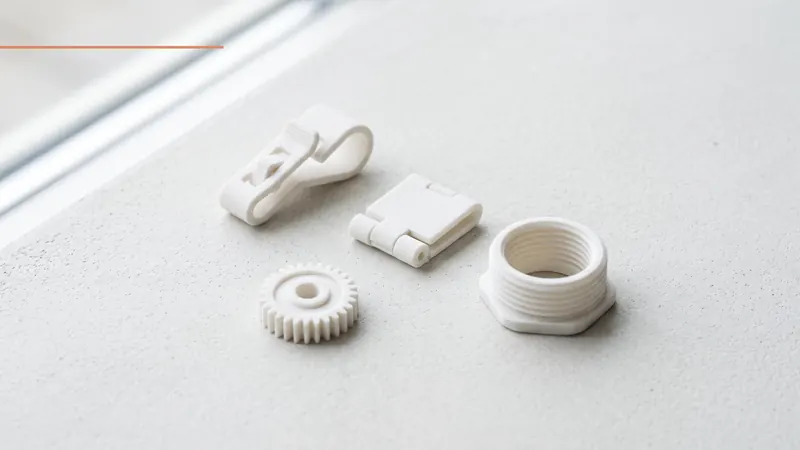
PA12, also written PA 12, nylon 12 or polyamide 12, is the standard material for powder-based 3D printing. This guide covers what it is, how laser-sintered PA12 nylon behaves and where it should not be used.
What PA12 is
PA12 is a semi-crystalline thermoplastic from the polyamide (nylon) family. The number 12 refers to the twelve carbon atoms in the repeating unit of the polymer chain. Compared with the more common PA6 and PA66, the chain contains fewer amide groups per unit of length. That single difference explains most of its behavior: PA12 absorbs much less water, keeps its dimensions better in humid conditions and resists more chemicals, at the price of lower stiffness and a lower melting point.
The names PA12, PA 12, nylon 12 and polyamide 12 all describe the same polymer. Trade names of sintering powders differ by manufacturer.
Why PA12 dominates SLS printing
Laser sintering needs a powder with a wide gap between the temperature at which it melts and the temperature at which it recrystallizes. Inside that window the powder bed can be kept hot without the parts solidifying unevenly, which keeps warping under control. PA12 has such a window, flows well as a powder and can be partly reused after a build. These processing properties, more than any single mechanical value, made it the default material for selective laser sintering.
Typical properties of laser-sintered PA12
The figures below are typical ranges published for laser-sintered PA12 powders. They are orientation values, not a specification. Actual values depend on the powder grade, the machine, the build orientation and the conditioning of the part. For design calculations use the datasheet of the specific powder.
| Property | Typical range, sintered PA12 | What it means in practice |
|---|---|---|
| Density of the sintered part | about 0.93 to 1.0 g/cm³ | Light; roughly a third of the density of aluminum |
| Tensile strength | about 45 to 50 MPa | Comparable with many molded engineering plastics |
| Tensile modulus | about 1,600 to 1,800 MPa | Stiff, but thin walls flex noticeably |
| Elongation at break | about 10 to 20 % | Enough ductility for snap-fits and clips |
| Melting point | about 175 to 180 °C | Well above normal service temperatures |
| Moisture absorption | low for a polyamide | Dimensions and stiffness stay stable in humid air |
Strength in the build direction is usually somewhat lower than within the layers, and elongation at break is the property that varies most between builds and orientations. A part that relies on a thin flexing feature should be tested, not only calculated.
Chemical and environmental behavior
- Oils, greases, fuels and hydrocarbons: generally good resistance, which is why PA12 is common in machine building and automotive development.
- Alkalis and many solvents: generally good resistance.
- Strong acids and oxidizing agents: not suitable.
- Water and humidity: low absorption compared with PA6. Sintered parts have some surface porosity, so thin walls are not automatically pressure-tight.
- Sunlight: untreated white PA12 can yellow and become more brittle after long outdoor exposure. For permanent outdoor use ask about suitable treatment or testing.
- Temperature: short exposure to elevated temperatures is tolerated, but stiffness falls as temperature rises. Check the heat deflection values in the datasheet against your load case.
Food contact, skin contact and medical use need documented evidence, not assumptions from the name of the polymer. For its PA 2200 powder, EOS states compliance with Regulation (EC) No 1935/2004 and GMP, and says its polymer materials are tested for cytotoxicity, sensitization, irritation and acute systemic toxicity; EOS also points out that the properties of a material allow no direct conclusion about a finished part. Sintered parts have a slightly porous surface that is harder to clean than a molded one, and dyeing adds another substance. Whether a finished part is fit for its use is the responsibility of whoever places it on the market. If your application needs such evidence, ask us before you order.
PA12 compared with related materials
| Material | Compared with sintered PA12 | Choose it when |
|---|---|---|
| PA11 | More ductile and impact-resistant, slightly less stiff; made from castor oil | Parts are bent repeatedly or take impacts |
| PA12 glass-filled | Stiffer and more heat-stable, more brittle, rougher | Stiffness under temperature matters more than toughness |
| PA6 / PA66 (molded or machined) | Stiffer and stronger, higher melting point, absorbs much more water | High loads and temperatures in a molded series part |
| TPU | Rubber-like, flexible | Seals, bellows, soft-touch elements |
| ABS (filament-printed) | Cheaper for simple shapes, clearly anisotropic, visible layers | Simple one-off parts with low loads |
White or gray: why base color matters
PA12 parts from laser sintering are white. PA12 parts from Multi Jet Fusion are gray because of the fusing agent used in that process. A white base can be dyed in light and saturated colors; a gray base is in practice limited to dark shades, most often black. If color is part of the requirement, decide on the process before you finalize the design. The article MJF vs SLS compares the two.
SLS Market dyes white PA 12 parts in any of 61 colors, in a separate optional step after blasting, with liquid dyes from the dye maker TCN; the shades are shown in the color catalog.
Designing parts in PA12
- Use the ductility. Snap-fits, clips and living-hinge-like features work if the strain is kept moderate and the feature is oriented within the layers where possible.
- Keep walls even. Uniform wall thickness of roughly 1.5 to 3 mm gives stable, economical parts. Typical minimum wall thickness is about 0.8 to 1.0 mm.
- Avoid solid blocks. Hollow thick sections and add escape holes for the powder.
- Plan threads. Large threads can be printed. For small or frequently used threads, threaded inserts or thread-forming screws for plastics are more durable.
- Allow for tolerance. The typical general tolerance for the process is ±0.3 %, with a lower limit of ±0.3 mm. Design fits with clearance or plan to rework critical bores.
Typical applications
Laser-sintered PA12 is used for functional prototypes, housings and covers, cable and hose guides, brackets, jigs and fixtures, gripper fingers for automation, air ducts, and small series or spare parts for machines. The common factor is a part that has to carry load or survive handling, in a quantity where a mold does not pay off.
When PA12 is the wrong material
- The part must be transparent or optically clear.
- It runs permanently at high temperature under load.
- It needs rubber-like flexibility.
- It is exposed to strong acids.
- It needs the stiffness of a metal or a fiber-reinforced composite.
PA12 at SLS Market
We print white Nylon PA 12 on an EOS FORMIGA P 110 Velocis and blast and surface the parts in a DyeMansion Powershot DUAL. Build volume, finishing options and ordering are described on the SLS 3D printing service page. An earlier, shorter overview of the material is available in SLS 3D Printing Nylon PA 12 (White).
Get an instant price
Upload STEP or STL files to the calculator and see the price of your parts in seconds: white Nylon PA 12, blasting and polishing included, optional dyeing in 61 colors, three delivery speeds. From there you send the order preview for confirmation.
Another material, an NDA or a large series? Write to us. For design help and prototype development see prototype.builders.
Get an instant price